Call us now :08071931606
 Send Inquiry
Quality Air Lock Valve


Quality Air Lock Valve Specification
- Pressure Type
- Medium Pressure
- Usage
- Industrial And Commercial
- Size
- Different Available
- Material
- Stainless Steel
- Color
- Silver
Quality Air Lock Valve Trade Information
- Minimum Order Quantity
- 1 Unit
- FOB Port
- India
- Payment Terms
- Cash Advance (CA), Cash in Advance (CID), Cheque
- Supply Ability
- 4 Units Per Month
- Delivery Time
- 1 Week
- Sample Available
- No
- Packaging Details
- Standard Packing
- Main Export Market(s)
- Australia, Asia, Central America, North America, South America, Eastern Europe, Western Europe, Middle East, Africa
- Main Domestic Market
- All India
Quality Air Lock Valve About
Airlock rotary valves, also frequently referred to as rotary airlocks, rotary feeders, or simply rotary valves, are essential components in bulk material handling systems.
Their primary function is to:
- Maintain pressure differentials:
- They act as a "lock" to prevent or minimize air loss between areas with differing pressures, whether in pneumatic conveying systems (pressure or vacuum) or other processes.
- Control material flow:
- They regulate the flow of dry, free-flowing bulk solids, such as powders, granules, and pellets, ensuring a consistent feed rate.
Applications:
- They are widely used in industries such as:
- Food processing
- Pharmaceuticals
- Chemical processing
- Plastics
- Agriculture
Types:
- Fall-Through Rotary Airlock Valve
- Blow-Through Rotary Airlock Valve
Engineered for Performance
Our air lock valves are meticulously crafted to meet stringent industrial standards. By utilizing stainless steel and a durable silver finish, these valves ensure excellent performance in medium-pressure environments. Choose from various sizes for a custom fit that enhances system reliability and reduces maintenance downtime.
Versatile Application Range
Designed for use across industrial and commercial sectors, these valves seamlessly integrate into processes such as pneumatic conveying, bulk material handling, and dust collection systems. Their versatility ensures efficiency and adaptability for a wide range of operational needs.
FAQ's of Quality Air Lock Valve:
Q: How is the Quality Air Lock Valve installed in a system?
A: Installation involves integrating the air lock valve into your existing pipeline or conveying system, ensuring the correct size and secure connections for optimal sealing performance. Professional installation by certified technicians is recommended for best results.Q: What are the main benefits of using a stainless steel air lock valve?
A: Stainless steel construction offers superior durability, corrosion resistance, and longevity. This ensures minimal maintenance and reliability even in demanding environments, ultimately reducing operational costs.Q: When should I replace or service my air lock valve?
A: Routine maintenance should be conducted based on system usage. Replacement or servicing is suggested if you notice signs of leakage, decreased efficiency, or visible wear, to maintain uninterrupted process operations.Q: Where can the air lock valve be used most effectively?
A: This valve is ideal for medium-pressure applications in industries such as food processing, pharmaceuticals, cement, and chemicals, where controlled handling of solid or granular materials is essential.Q: What is the process for selecting the correct valve size for my application?
A: Selection involves evaluating your system's flow rate, pressure requirements, and material characteristics. Our technical team can assist in recommending the ideal size to ensure compatibility and system optimization.Q: How does the air lock valve enhance process efficiency?
A: By maintaining a consistent pressure seal while managing the controlled flow of materials, the air lock valve minimizes material loss and ensures steady system pressure, improving overall operational efficiency.Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

More Products in Air Lock Valve Category
MS Rotary Airlock Valves
Price 35000 INR / Unit
Minimum Order Quantity : 1 Unit
Pressure Type : Other, Positive or Negative Pressure Applications
Material : Other, Mild Steel (MS)
Structure : Other, Rotary Valve with flange connection, motor and gearbox assembly
Pressure : Other, Up to 1 bar (customized available)
Rotary Air Lock Valves
Price 35000 INR / Unit
Minimum Order Quantity : 1 Unit
Pressure Type : Other, Positive / Negative (Vacuum) applications
Material : Other, Cast Iron, Mild Steel, Stainless Steel (SS304 / SS316 as per requirement)
Structure : Other, Rotary feeder with housing & rotor
Pressure : Other, Up to 1 bar (max) / Depending on process need
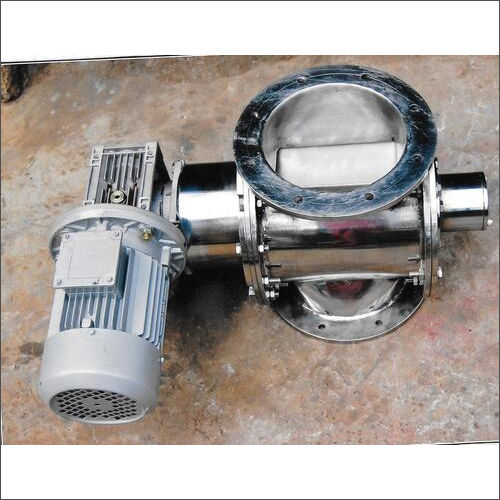
Industrial Air Lock Valve
Price 150000.00 INR / Unit
Minimum Order Quantity : 1 Unit
Pressure Type : High Pressure
Material : Stainless Steel
Structure : Diaphragm
Pressure : High Pressure mpa
Multi Purpose Air Lock Roatry Valves
Price 30000 INR / Unit
Minimum Order Quantity : 1 Unit
Pressure Type : Other, Low Pressure
Material : Other, Cast Iron, Mild Steel, Stainless Steel
Structure : Other, Rotary Valve
Pressure : Other, 0.6 MPa (Max)


 Send Inquiry
Our Products

I-8, Phase-II, GIDC, Near Vinzol Railway Crossing, Vatva,Ahmedabad - 382445, Gujarat, India

Mr Manoj Singh Rajput
(Proprietor)
Mobile :08071931606
 Send Inquiry
 Send SMS

Developed and Managed by Infocom Network Private Limited.
