Call us now :08071931606
 Send Inquiry
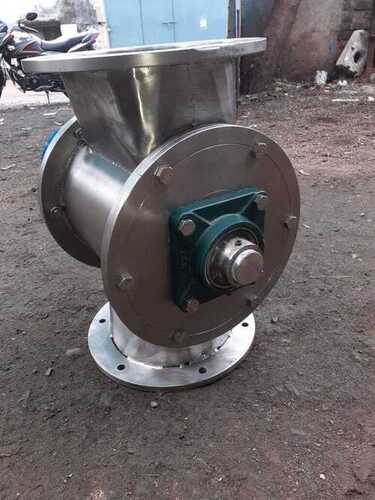
MS Rotary Airlock Valves
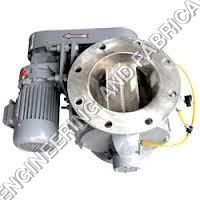

MS Rotary Airlock Valves Specification
- Port Size
- 100 mm / 150 mm / 200 mm / 300 mm and above
- Body Material
- Cast Iron or Mild Steel
- Pressure Type
- Positive or Negative Pressure Applications
- Media
- Powder, Granule, Dust, Pellet, Grain, etc.
- Application
- Used in pneumatic conveying systems, dust collection, silo discharge, bag filter discharge
- Dimension (L*W*H)
- Varies as per model (e.g. 450 x 300 x 350 mm approx.)
- Working Temperature
- Up to 150C (depends on gasket and seal type)
- Usage
- Industrial
- Material
- Mild Steel (MS)
- Power
- 0.5 HP to 5 HP (customizable as per requirement)
- Pressure
- Up to 1 bar (customized available)
- Structure
- Rotary Valve with flange connection, motor and gearbox assembly
- Size
- 100 mm to 450 mm (available in various sizes)
- Color
- Silver
- Weight
- Approx. 40 - 175 kg depending on size
- Drive Type
- Direct coupled or chain driven
- Rotor Type
- Closed or open design (customizable as per application)
- End Cover
- Removable for easy maintenance
- Surface Finish
- Painted or powder coated for anti-corrosion
- Speed
- 10 - 30 RPM (as per application)
- Customization
- Capacity, flange type, and material can be customized as per requirement
- Mounting
- Flanged/Foot Mounted
- Sealing
- Packing seal/air purge available
- Number of Vanes
- Usually 6-8 vanes
MS Rotary Airlock Valves Trade Information
- Minimum Order Quantity
- 1 Unit
- Supply Ability
- 50 Units Per Day
- Delivery Time
- 2 Months
- Main Domestic Market
- All India
MS Rotary Airlock Valves About
Experience the sensational performance of our Best-selling MS Rotary Airlock Valves-engineered for monumental reliability in industrial applications. With reserve options for direct coupled or chain-driven mechanisms, these premier rotary valves offer customizable closed or open rotors and adaptable sealing solutions for any material and process requirement. The robust mild steel body, removable end covers, and exceptional anti-corrosion finishes guarantee lasting freshness and easy maintenance. Available in various sizes, capacities, and power configurations, they are designed for powder, granule, dust, and pellet media under both positive and negative pressure environments. Elevate your conveying process with this fresh, high-performance solution.
Versatile Applications & Standout Features
The MS Rotary Airlock Valves deliver premier performance for both specific and general industrial uses, thriving in pneumatic conveying systems, dust collection units, and silo or bag filter discharges. Their monumental design allows operation on various surfaces, from factory floors to process lines, accommodating powders, grains, and pellets. Key extra features include easy-flange mounting, powder-coated anti-corrosion surfaces, air purge sealing, and capacity for custom-built solutions-making these rotary valves a sensational choice for manufacturers and service providers alike.
Delivery Timelines, Payment Criteria, and Export Market Reach
Orders for MS Rotary Airlock Valves are processed promptly to ensure swift delivery-most models are delivered within a competitive rate frame, depending on specification and customization. Secure payment terms are accepted, tailored to suit your company's financial process requirements. Our premier valves regularly arrive in major export markets across Asia, Africa, and the Middle East, with customer satisfaction supported by streamlined logistics and reliable shipping partners, ensuring on-time arrival and safe handling regardless of destination.
Versatile Applications & Standout Features
The MS Rotary Airlock Valves deliver premier performance for both specific and general industrial uses, thriving in pneumatic conveying systems, dust collection units, and silo or bag filter discharges. Their monumental design allows operation on various surfaces, from factory floors to process lines, accommodating powders, grains, and pellets. Key extra features include easy-flange mounting, powder-coated anti-corrosion surfaces, air purge sealing, and capacity for custom-built solutions-making these rotary valves a sensational choice for manufacturers and service providers alike.
Delivery Timelines, Payment Criteria, and Export Market Reach
Orders for MS Rotary Airlock Valves are processed promptly to ensure swift delivery-most models are delivered within a competitive rate frame, depending on specification and customization. Secure payment terms are accepted, tailored to suit your company's financial process requirements. Our premier valves regularly arrive in major export markets across Asia, Africa, and the Middle East, with customer satisfaction supported by streamlined logistics and reliable shipping partners, ensuring on-time arrival and safe handling regardless of destination.
FAQ's of MS Rotary Airlock Valves:
Q: How do MS Rotary Airlock Valves enhance pneumatic conveying applications?
A: MS Rotary Airlock Valves facilitate uninterrupted, accurate transfer of materials such as powder, granule, and pellets between system components, ensuring consistent pressure control and preventing air leakage in pneumatic conveying processes.Q: What customization options are available for these rotary airlock valves?
A: Customers can tailor rotor design (open or closed), flange types, body material (cast iron or mild steel), surface finish, capacity, and power specifications to precisely fit unique material handling requirements and site conditions.Q: When should packing seal or air purge options be selected?
A: Packing seal is ideal for standard applications, while air purge sealing is recommended for handling fine or sticky materials, high-temperature operations, or when preventing product leakage or contamination is crucial.Q: Where can MS Rotary Airlock Valves be installed?
A: They are commonly installed in bag filter discharges, silo outputs, dust collector exits, or at points where controlled feeding and isolation of media in positive or negative pressure systems are essential.Q: What is the process for selecting the right valve size and configuration?
A: Selection involves evaluating media type, required rate of flow, pressure, temperature, and system connection needs. Our technical team assists clients in determining the most suitable model by analyzing operational parameters and desired performance.Q: What benefits do removable end covers and anti-corrosion coating offer?
A: Removable end covers enable convenient cleaning and maintenance, reducing downtime. Anti-corrosion painted or powder-coated surfaces extend the valve's operational life and ensure reliable function in harsh industrial environments.Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

More Products in Air Lock Valve Category
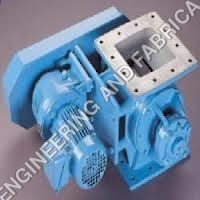
Rotary Air Lock Valves
Price 35000 INR / Unit
Minimum Order Quantity : 1 Unit
Material : Other, Cast Iron, Mild Steel, Stainless Steel (SS304 / SS316 as per requirement)
Pressure Type : Other, Positive / Negative (Vacuum) applications
Color : Blue
Size : Customizable as per process requirements
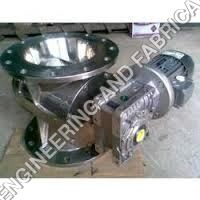
Multi Purpose Air Lock Roatry Valves
Price 30000 INR / Unit
Minimum Order Quantity : 1 Unit
Material : Other, Cast Iron, Mild Steel, Stainless Steel
Pressure Type : Other, Low Pressure
Size : 2 to 24 (custom sizes available)
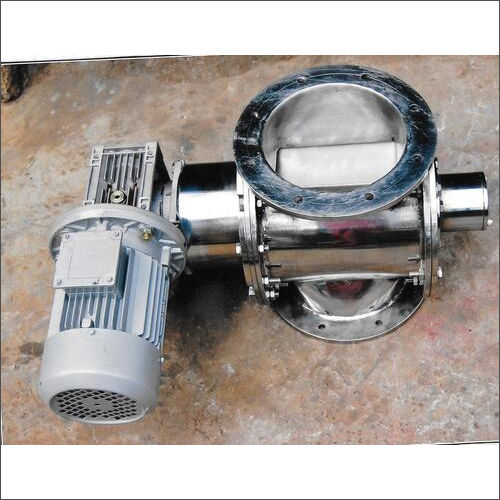
Industrial Air Lock Valve
Price 150000.00 INR / Unit
Minimum Order Quantity : 1 Unit
Material : Stainless Steel
Pressure Type : High Pressure
Color : Silver
Round Air Lock Valve
Price 50000 INR / Unit
Minimum Order Quantity : 1 Unit
Material : Stainless Steel
Pressure Type : High Pressure
Color : Silver
Size : Different Available


 Send Inquiry
Our Products

I-8, Phase-II, GIDC, Near Vinzol Railway Crossing, Vatva,Ahmedabad - 382445, Gujarat, India

Mr Manoj Singh Rajput
(Proprietor)
Mobile :08071931606
 Send Inquiry
 Send SMS

Developed and Managed by Infocom Network Private Limited.
